Cat Carrier Collapsible: Storage Friendly
A collapsible cat carrier should store at 22-30% of its deployed volume and re-erect in under 20 seconds with no tools, while still holding floor deflection under 5 mm at a 10 kg load. That needs reinforced foldable ribs at 12-18 mm depth on a 90-140 mm pitch, articulated joints rated to 2,000 fold cycles, and a lock that holds the erected state without operator skill.
This page sets out how a collapsible cat carrier is engineered so that the storage benefit does not arrive as a structural cost. Collapsibility and rigidity pull in opposite directions: every articulation is a discontinuity in the load path, and a carrier that folds flat tends to flex where it was never meant to. The resolution used in production is a reinforced foldable rib — a rib that carries load when erected and folds at a controlled point when released — combined with a lock that transfers load across the articulation rather than through it. Section by section, this page covers the collapse mechanism options, rib geometry, the articulation detail and its fatigue life, the freight arithmetic, and the cycle testing that separates a durable folding product from one that fails in the second season. Commercial terms follow the standard programme: MOQ 500 pieces per colourway, prototypes in 6-10 working days, bulk production 35-50 days after sample approval, final random inspection to AQL 2.5, T/T 30/70 and FOB Xiamen.
Wholesale pet carrier programmes for cat carrier ranges run 35-50 days after sample approval, shipped FOB Xiamen under T/T 30/70 terms.
Collapse Mechanisms Compared: Hoop Twist, Frame Release and Rib Fold
Three mechanisms account for nearly all collapsible cat carriers on the market, and they differ in how much structure they give up. Choosing between them is the first decision and the one that constrains everything downstream, because the mechanism determines where the load path is interrupted.
Hoop twist is the lightest and simplest. A continuous spring rod or a pair of rods in a sleeve is twisted into a figure-of-eight and the carrier folds into two flat loops, exactly as a pop-up laundry hamper does. It collapses to roughly 20-25% of deployed volume, adds 60-140 g, and gives up almost all rigid structure: the floor is unsupported, the walls are membrane-tensioned only, and the product relies entirely on the rod's pre-load. It suits short-duration use with a calm cat and does not suit a carrier that has to hold a shape under an animal that braces.
Frame release is the opposite extreme. A rigid or semi-rigid frame — moulded polymer uprights or a wire frame with corner joints — is released at four or more points and folds down, with the floor board remaining rigid. Deployed structural performance is close to a non-collapsible carrier, collapsed volume is 30-40%, and the mechanism adds 220-420 g and 2.60-6.40 USD. Re-erection takes 30-60 seconds and requires the operator to understand the mechanism, which is a real retail objection.
| Mechanism | Collapsed volume | Added mass (g) | Added cost (USD) | Erection time | Structural penalty |
|---|---|---|---|---|---|
| Hoop twist | 20-25% | 60-140 | 0.60-1.60 | Under 10 s | High |
| Rib fold, unreinforced | 24-32% | 110-200 | 1.40-3.20 | 10-20 s | Medium |
| Rib fold, reinforced | 26-34% | 170-290 | 2.40-5.20 | 15-25 s | Low |
| Frame release | 30-40% | 220-420 | 2.60-6.40 | 30-60 s | Very low |
Rib fold is the middle route and the one this page concentrates on. Vertical or circumferential ribs carry load when erected and fold at discrete articulated points when released, giving a collapsed volume of 24-34% with most of the deployed rigidity retained. The engineering cost is that every fold point is a fatigue site, and the fatigue life of the articulation — not the strength of the rib — is what determines the product's service life.
Selection should follow the use case rather than the collapsed number. A carrier bought for occasional vet trips and stored under a bed wants the deepest collapse and can accept the structural penalty. A carrier bought for regular travel wants rigidity and can accept 34%. The collapse ratio is a marketing number; the structural penalty is the engineering one.
Reinforced Foldable Rib Design: Section, Pitch and Articulation
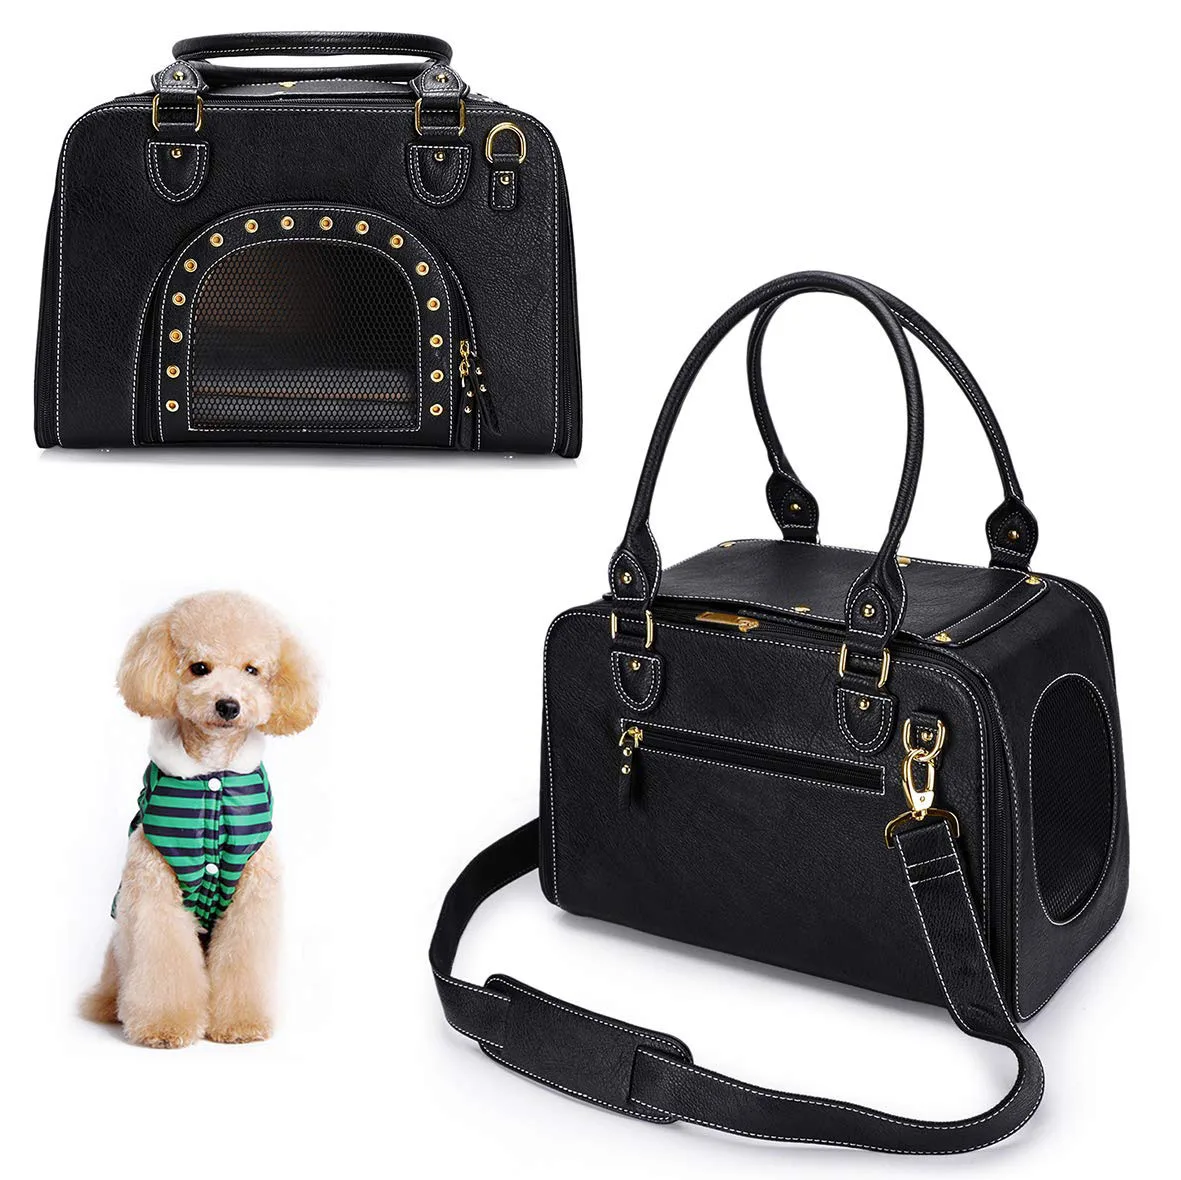
A foldable rib has to do two incompatible things: behave as a continuous stiffener when the carrier is erected, and become a hinge at a known location when it is folded. The design that satisfies both is a rib whose section is constant along its length but whose articulation is a discrete, reinforced joint — not a rib that is simply thinner at the fold, which is the common and wrong approach.
Rib section comes first. For the cat class, a rib of 12-18 mm depth with a wall of 1.2-2.0 mm in PP or a moulded polymer gives a section modulus sufficient to hold the wall panels in tension without adding a separate frame. Pitch is set by the panel span: 90-140 mm between ribs on a 450-550 mm panel keeps the fabric between them from billowing under load while leaving enough unsupported area for the carrier to fold. A tighter pitch improves rigidity and makes folding worse; a wider pitch does the reverse.
The articulation is a discrete component rather than a thinned section. Three constructions are used: a moulded living hinge in PP with a 0.4-0.8 mm web, a two-part polymer knuckle with a 3-4 mm pin, and a textile hinge of 40-60 mm webbing bridging the rib ends. The living hinge is cheapest and folds the flattest but cannot be used in ABS or in glass-filled materials, and its fatigue life is sensitive to moulding conditions. The knuckle is the most durable at 1.20-3.00 USD per joint and is the specification for programmes claiming a long service life.
Reinforcement at the joint is what turns a folding rib into a load-carrying one. In the erected state the joint is not loaded in bending if the rib is locked, but it is loaded in bending during erection and whenever the carrier is handled partly folded. The control is an over-centre geometry: the rib passes slightly beyond straight at full erection so load drives it into a stop rather than into the joint. Combined with a locking sleeve that slides over the joint, an over-centre rib carries 60-80% of the load an uninterrupted rib would.
Stop faces and travel limits close the design. A folding rib without a positive stop will over-travel, put its joint into reverse bending, and fail at a few hundred cycles instead of a few thousand. The stop should be a moulded face of at least 40 mm² bearing area, and the over-travel allowance should be 1-2 degrees rather than 5-10. A foldable rib is a stiffener with a controlled discontinuity; the discontinuity has to be designed, not thinned into existence.
Articulation Detail: Fatigue Life and Failure Modes
The articulation is the life-limiting component in a collapsible carrier, and it fails by fatigue at loads far below its static strength. Understanding the failure mode matters more than knowing the load figure, because the two usual modes have opposite remedies.
A living hinge in polypropylene fails by crack initiation at the hinge root, driven by the strain imposed at each fold. That strain is a function of the web thickness and the fold angle: a 0.5 mm web folded through 170 degrees imposes roughly 3% strain and survives 15,000-40,000 folds; a 0.8 mm web under the same fold imposes closer to 5% and survives 3,000-8,000. The counter-intuitive conclusion is that thinner hinges last longer, and the practical limit is set by the moulding process rather than by design.
A knuckle joint fails differently — by wear at the pin bore and by elongation of the bore under repeated load. The remedy is a bushing or a bearing surface: a moulded polymer knuckle with a steel pin of 3-4 mm and a bore length of at least 1.5 x pin diameter survives 20,000-50,000 folds, while the same joint without adequate bore length frets and loosens in 2,000-5,000. Pin retention is the associated detail and should be positive — a headed pin, a circlip or a moulded cap — rather than a friction fit.
Textile hinge failure is progressive and visible, which makes it preferable in some programmes. The webbing bridge abrades at its fold line and eventually tears, and the failure is preceded by visible fraying. A 50 mm webbing bridge of 600-900 g/m² polyester with a bound fold at 20-25 mm survives 8,000-15,000 folds and gives warning before it fails. For a consumer product, a visible wear indicator is a genuine advantage over a sudden polymer fracture.
Contamination accelerates every one of these modes. Cat hair and litter dust work into a knuckle bore and act as an abrasive, and dried moisture stiffens a textile hinge and raises its fold strain. A design review should ask whether the articulation is exposed to the interior; where it is, a shroud of 20-30 mm of fabric over the joint costs almost nothing and extends life measurably.
Verification is a fold cycle test rather than a calculation. A fixture folding the carrier fully and re-erecting it at 6-10 cycles per minute, to 2,000 cycles for occasional-use products and 5,000-10,000 for travel products, with inspection at 25%, 50% and 100% of the run. Acceptance is no crack, no measurable bore elongation above 0.2 mm, and no loss of erected shape. Fatigue life, not static strength, is the specification that determines whether a collapsible carrier lasts one season or five.
Collapsed Volume Ratio and the Freight Arithmetic
The stated benefit of collapsibility is storage; the financial benefit is usually freight. Both are worth calculating properly, because the arithmetic determines whether the mechanism pays for itself, and the answer depends on where in the supply chain the collapse happens.
Collapsed volume ratio is measured as collapsed external volume divided by deployed external volume, calculated from the bounding box of each state rather than from the interior volume. For a rib-fold cat carrier the figure is typically 26-34%; the corresponding deployed volume for the cat class is 55-70 litres of bounding box, giving a collapsed box of 15-24 litres. The published collapse ratio should always state which two volumes it compares, because the ratio calculated against interior volume is 15-20 percentage points more flattering and is the one usually quoted.
| State | Units per 0.09 m³ carton | Cartons per 500 units | Volume (m³) | Freight index |
|---|---|---|---|---|
| Deployed, boxed | 4-6 | 83-125 | 7.5-11.3 | 100 |
| Collapsed, boxed | 10-14 | 36-50 | 3.2-4.5 | 42-58 |
| Collapsed, nested in master | 14-18 | 28-36 | 2.5-3.2 | 33-43 |
That 42-58% freight index is the real argument for collapsibility, and at typical sea rates it is worth 1.80-4.20 USD per unit — more than the mechanism costs. The caveat is that the saving only materialises if the product ships collapsed. If the retailer wants shelf-ready deployed units, the benefit disappears and the mechanism becomes a pure cost, which is why the shipping state should be agreed at quotation rather than assumed.
Storage benefit is smaller and more subjective but still worth quantifying. A deployed cat carrier occupies 55-70 litres of cupboard space, which most households do not have; a collapsed one occupies 15-24 litres and fits under a bed or on a shelf. Retail display is the other side of the same arithmetic: a collapsible carrier can be displayed deployed with a collapsed unit alongside, which communicates the feature without costing floor space.
Warehousing at the brand end is the third and least discussed effect. A brand holding 2,000 units of a collapsible carrier uses roughly a third of the racking of a non-collapsible equivalent, which for a DTC operation paying by pallet position is a recurring saving rather than a one-off. Collapsibility pays for itself in freight or not at all — the storage benefit alone rarely justifies the mechanism.
Re-Erection Force, Shape Recovery and Memory After Storage
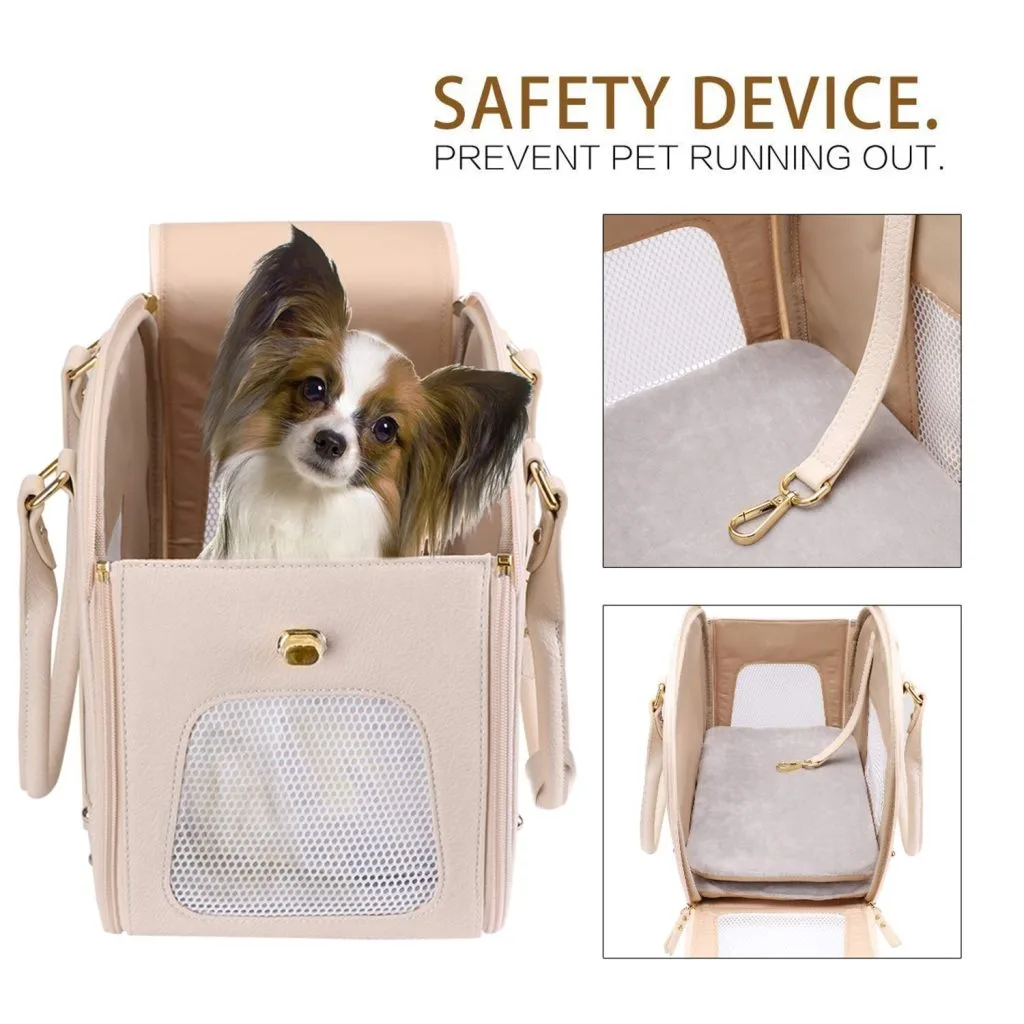
A collapsible carrier has to be erected by a customer who has not read the instructions, usually with a cat waiting. The ergonomics of that operation are as much a specification as the structure, and they are almost never measured.
Re-erection force is the first measurable. For a rib-fold mechanism the peak force should fall between 30 and 90 N and the total work per erection under 12 joules; above those figures the operation feels stiff and customers report it as a defect. Force is dominated by the fabric panel tension rather than by the mechanism, so a carrier that is hard to erect is usually over-tensioned at the panels rather than over-spec'd at the ribs.
Erection time is the second. A measurable and defensible target is under 20 seconds for a first-time user working from the printed instruction sheet, and under 8 seconds for a user who has done it before. Timing a naïve user is the only way to get a real number; an engineer who has erected the sample forty times will report 4 seconds and learn nothing.
Shape recovery after storage is the third and the one that produces complaints. A carrier stored collapsed for months takes a set: the fabric creases, the ribs hold a partly folded memory, and the erected product does not reach its designed volume. The control is twofold — store the ribs in a relaxed rather than a stressed state, which argues for a rib that folds to straight rather than to a tight radius, and specify a recovery acceptance test.
The recovery test is simple and worth running: collapse the carrier, store it at 23 °C for 30 days under a 2 kg load, erect it, and measure interior volume after 60 seconds and after 24 hours. Acceptance is 95% of nominal volume at 60 seconds and 100% at 24 hours. A product that needs 24 hours to recover will be returned by a customer who needed it in 20 seconds.
Instruction design is part of the engineering. A mechanism that requires the operator to release four catches in a sequence needs a numbered, illustrated sequence on a hang tag that stays with the product, not a folded sheet that is discarded. Erection is an ergonomic operation with a measurable force, a measurable time and a measurable recovery, and all three belong on the specification.
Recovering the Structural Performance Lost to Collapsibility
Every articulation removes stiffness, and the engineer's job is to buy that stiffness back somewhere cheaper than the joint. Four techniques recover most of the loss, and they are worth applying in order because the first two are close to free.
The first is the over-centre lock described earlier: geometry that drives the rib into a stop under load rather than into the joint. It costs nothing in parts and recovers 25-40% of the lost stiffness. The second is a locking sleeve — a moulded or fabric sleeve of 40-80 mm that slides over the articulation in the erected state and is held by hook-and-loop or a snap. At 0.20-0.60 USD per joint it recovers another 20-30% and, importantly, keeps the joint aligned if the carrier is handled roughly while erected.
The third technique is a tensioned perimeter. A webbing or cord of 3-4 mm run around the carrier's erected perimeter and tensioned at erection puts the whole shell into membrane tension, so panels and ribs share load. It adds 40-90 g and 0.40-1.10 USD and is the most effective single addition for a hoop-twist or lightly ribbed structure, recovering enough rigidity to bring floor deflection back inside 5 mm at a 10 kg load.
The fourth is a removable rigid floor board. Because the floor is the surface the cat actually loads, and because a board can be inserted at erection and removed for collapse without any articulation at all, a rigid board buys back the most important structural property for 1.10-2.90 USD with no fatigue penalty. Programmes that combine a tensioned perimeter with a removable board typically land within 10-15% of a non-collapsible carrier's measured performance.
Verification closes the loop. The structural protocol — floor deflection, handle pull, drop, shape retention — is run on the collapsible sample in its erected state and compared against a non-collapsible reference of the same volume. The comparison should be recorded as a percentage rather than a pass/fail, because the trade is a design decision that the brand should make knowingly rather than discover. Collapsibility costs stiffness at each joint; the cost is recoverable, but only if it is measured and paid for deliberately.
Fold Cycle Testing and Acceptance Criteria
Fold cycle testing is the acceptance gate for a collapsible design, and it should be run on complete production-representative carriers rather than on joint coupons. A coupon test measures the joint; a product test measures the joint plus the fabric tension, the panel alignment and the operator-induced misalignment that actually causes failures.
The protocol runs a full collapse-and-erect cycle at 6-10 cycles per minute, driven by a fixture that pulls at the designed handle points rather than at arbitrary locations. Two thousand cycles is the acceptance target for occasional-use products and 5,000-10,000 for travel products. Inspection happens at 25%, 50% and 100% of the run, and the recorded values are fold force, erected interior volume, floor deflection and any visible damage at the articulations.
Acceptance limits: no crack or tear at any articulation, pin bore elongation under 0.2 mm, fold force drift under 25% of the initial value, erected volume loss under 5%, and floor deflection still under 5 mm at 10 kg. Two units are additionally inspected destructively at the end of the run, with the articulations sectioned to check for crack initiation that has not yet reached the surface.
Conditioning sets complete the protocol. One set runs at -10 °C after four hours of conditioning, where polypropylene living hinges and coated fabrics both stiffen; another runs at 50 °C and 85% relative humidity for 48 hours, which softens coatings and raises fold strain. Both are 300-cycle sets, and both catch failures that a room-temperature run of 2,000 cycles will not.
Method references for conditioning and fatigue practice follow published standards work at ASTM International, and quality-system requirements for the production base are maintained to ISO 9001. Our production team records measured values at each inspection point rather than pass/fail outcomes, so that a mechanism drifting towards its limit is visible before it starts failing in the field.
Cost, Tooling and Programme Notes
A collapsible mechanism adds 2.40-6.40 USD to unit cost depending on the route, against a freight saving of 1.80-4.20 USD per unit when the product ships collapsed. The decision therefore turns on the shipping state, and that should be settled before the mechanism is chosen rather than after. Where the retailer requires deployed shelf-ready units, the cheaper answer is usually a non-collapsible carrier with a nested carton rather than a collapsible one shipped erected.
Tooling is the schedule driver for rib-fold designs. A moulded rib with a knuckle joint needs a tool of 12,000-26,000 USD on a nine to thirteen week path, and the joint detail is the part that usually needs a second iteration. Programmes working to a fixed launch date should consider a textile-hinge rib, which needs only a die tool at 800-2,200 USD and can be revised between sample rounds at almost no cost.
Assembly cost is higher than the parts cost suggests. A rib-fold carrier takes 60-120 seconds more per unit to assemble than a plain one, because the articulations have to be aligned and the locking sleeves fitted by hand rather than by machine. On a 500-piece order at MOQ that is 8-17 additional line-hours, and it is the reason collapsible carriers carry a higher labour content than their component count implies.
Retail presentation carries the argument for the feature. A collapsed unit shown beside an erected one communicates the benefit in a way that copy cannot, and the packaging should state the collapsed dimension and the erection time as numbers. Schedule and commercial terms are standard: prototypes in 6-10 working days, bulk production 35-50 days after sample approval, final random inspection to AQL 2.5 with fold-cycle and erected-dimension checks added to the defect list, T/T 30/70 and FOB Xiamen. Collapsibility is a freight and storage decision with a structural price; the price is worth paying when the shipping state cooperates.
Why brands source here
- Pet carrier programs run since 2014; founding team in sewn goods since 2004
- SGS-verified production floor of 4,950 m² with 137 workers across 7 lines
- Monthly capacity of 200,000 units, audited to BSCI and ISO 9001
People Also Ask
How flat should a collapsible cat carrier fold?
To 22-30% of its deployed bounding-box volume, typically 15-24 litres from a 55-70 litre deployed box. Always check whether a quoted ratio compares bounding boxes or interior volumes — the interior comparison flatters by 15-20 points.
What is a reinforced foldable rib?
A rib of 12-18 mm depth that carries load when erected and folds at a discrete articulated joint, with over-centre geometry that drives load into a stop rather than the joint. Combined with a locking sleeve it carries 60-80% of an uninterrupted rib's load.
Why not simply thin the rib at the fold?
A thinned section is a stress concentrator with no defined fold axis and no fatigue life worth quoting. A discrete joint — living hinge, knuckle or textile bridge — gives a controlled fold point and a measurable cycle life.
How many fold cycles should a collapsible carrier survive?
2,000 for occasional-use products and 5,000-10,000 for travel products, with inspection at 25%, 50% and 100% of the run and destructive sectioning of two units at the end.
How much freight does collapsing actually save?
A freight index of 42-58% against deployed shipping, worth 1.80-4.20 USD per unit at typical sea rates, and 33-43% if units are nested in a master carton. The saving disappears if the retailer requires deployed units.
How long should erection take?
Under 20 seconds for a first-time user working from the instruction sheet and under 8 seconds for an experienced one, with peak fold force between 30 and 90 N and total work under 12 joules.
How is stiffness recovered after adding articulations?
Over-centre geometry, a locking sleeve at 0.20-0.60 USD per joint, a tensioned perimeter cord at 40-90 g, and a removable rigid floor board. The perimeter and the board together bring performance within 10-15% of a non-collapsible reference.
Frequently Asked Questions
Which collapse mechanism suits a travel carrier?
A reinforced rib fold at 26-34% collapsed volume with a removable rigid floor board. Hoop twist gives up too much structure for regular travel, and frame release is heavy and slow to erect at 30-60 seconds.
What rib pitch is recommended for a 450-550 mm panel?
90-140 mm. A tighter pitch improves rigidity and makes folding worse; a wider pitch allows the fabric to billow under load.
Why does a thinner living hinge last longer?
Fold strain falls with web thickness. A 0.5 mm web folded through 170 degrees imposes about 3% strain and survives 15,000-40,000 folds; a 0.8 mm web imposes closer to 5% and survives 3,000-8,000.
Can a living hinge be used with ABS or glass-filled material?
No. Living hinges are a polypropylene feature. ABS and glass-filled grades require a knuckle joint with a steel pin of 3-4 mm or a textile hinge bridge.
What makes a knuckle joint durable?
Bore length of at least 1.5 x pin diameter, a positive pin retention method such as a headed pin or circlip, and protection from contamination. With those, 20,000-50,000 folds are achievable; without them the joint frets loose in 2,000-5,000.
Why is a textile hinge sometimes preferable?
It fails visibly. A 50 mm webbing bridge of 600-900 g/m² polyester with a bound fold survives 8,000-15,000 folds and frays before it tears, giving the owner warning rather than a sudden fracture.
How should articulations be protected from contamination?
With a fabric shroud of 20-30 mm over the joint where it is exposed to the interior. Cat hair and litter dust act as an abrasive in a knuckle bore and dried moisture raises fold strain in a textile hinge.
What stop geometry is required on a folding rib?
A moulded face of at least 40 mm² bearing area with an over-travel allowance of 1-2 degrees. A rib without a positive stop over-travels, reverse-bends its joint and fails in hundreds of cycles.
How is shape recovery after storage tested?
Collapse the carrier, store it at 23 °C for 30 days under a 2 kg load, erect it and measure interior volume at 60 seconds and 24 hours. Acceptance is 95% of nominal at 60 seconds and 100% at 24 hours.
What does a tensioned perimeter add?
40-90 g and 0.40-1.10 USD, and it puts the whole shell into membrane tension so panels and ribs share load. It is the most effective single addition for a lightly ribbed structure.
Why is the floor board kept removable?
Because the floor is the surface the cat actually loads and a board needs no articulation at all. It buys back the most important structural property for 1.10-2.90 USD with no fatigue penalty.
What are the fold cycle acceptance limits?
No crack or tear, pin bore elongation under 0.2 mm, fold force drift under 25%, erected volume loss under 5%, and floor deflection still under 5 mm at 10 kg.
Why run low- and high-temperature conditioning sets?
Polypropylene hinges and coated fabrics stiffen at -10 °C, while coatings soften at 50 °C and 85% relative humidity, raising fold strain. Both conditions produce failures a room-temperature run misses.
What tooling does a rib-fold mechanism need?
12,000-26,000 USD and nine to thirteen weeks for a moulded rib with a knuckle joint, usually with a second iteration on the joint detail. A textile-hinge rib needs only a die tool at 800-2,200 USD.
Talk to QUANZHOU JUNYUAN BAGS about a pet carrier program: MOQ 500 pieces per colourway, samples in 6-10 working days, bulk production in 35-50 days under AQL 2.5 inspection.
Get a free quote Request a sample